We automate chemicals material handling.
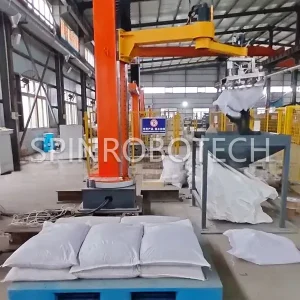
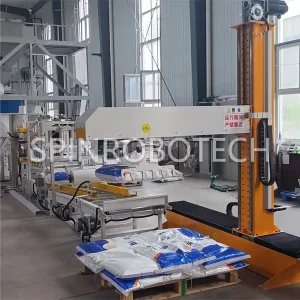
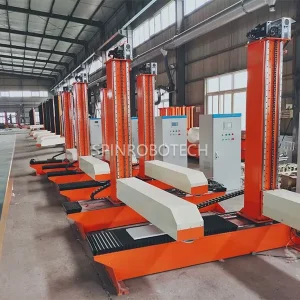
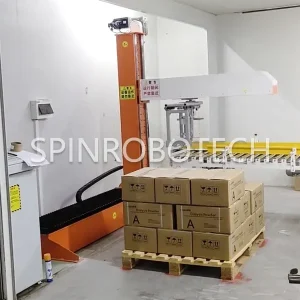
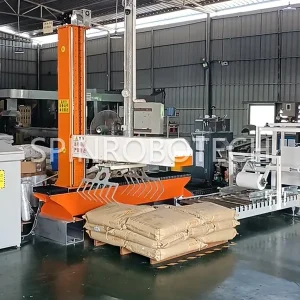
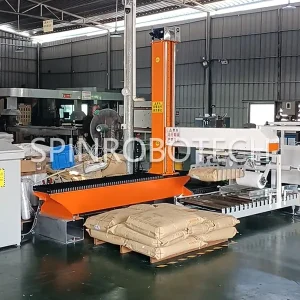
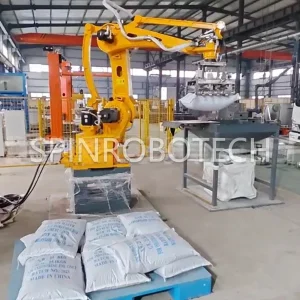
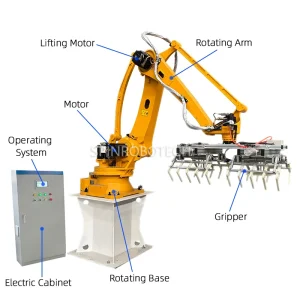
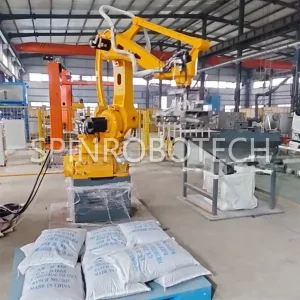
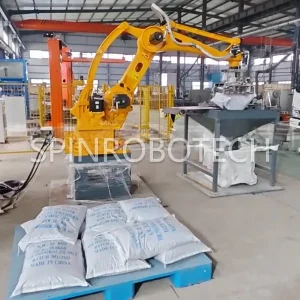
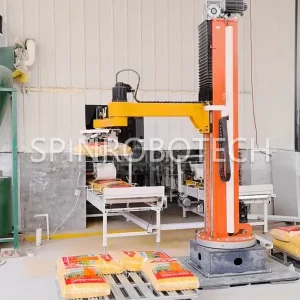
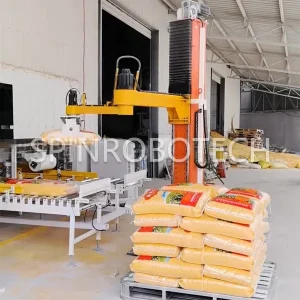
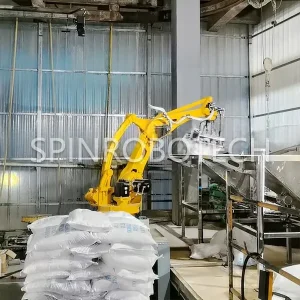
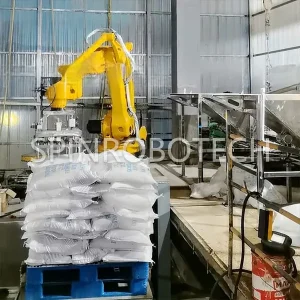
Palletizers stack bags, boxes, and drums.
Depalletizers unload incoming raw materials.
Stretch wrappers and banders secure each layer.
Hooders apply protective covers for storage.
Mist fogging suppresses dust at transfer points.
Humidification prevents caking and static buildup.
Systems are built with corrosion‑resistant materials.
Explosion‑proof components protect volatile areas.
Sealed designs contain fine powders safely.
Quick changeovers handle different container sizes.
Sensors verify weight and stack integrity.
All integrates with your conveyor network.
Remote monitoring tracks performance in real time.
We provide full installation and training.
Contact us for a safe, efficient chemical line.